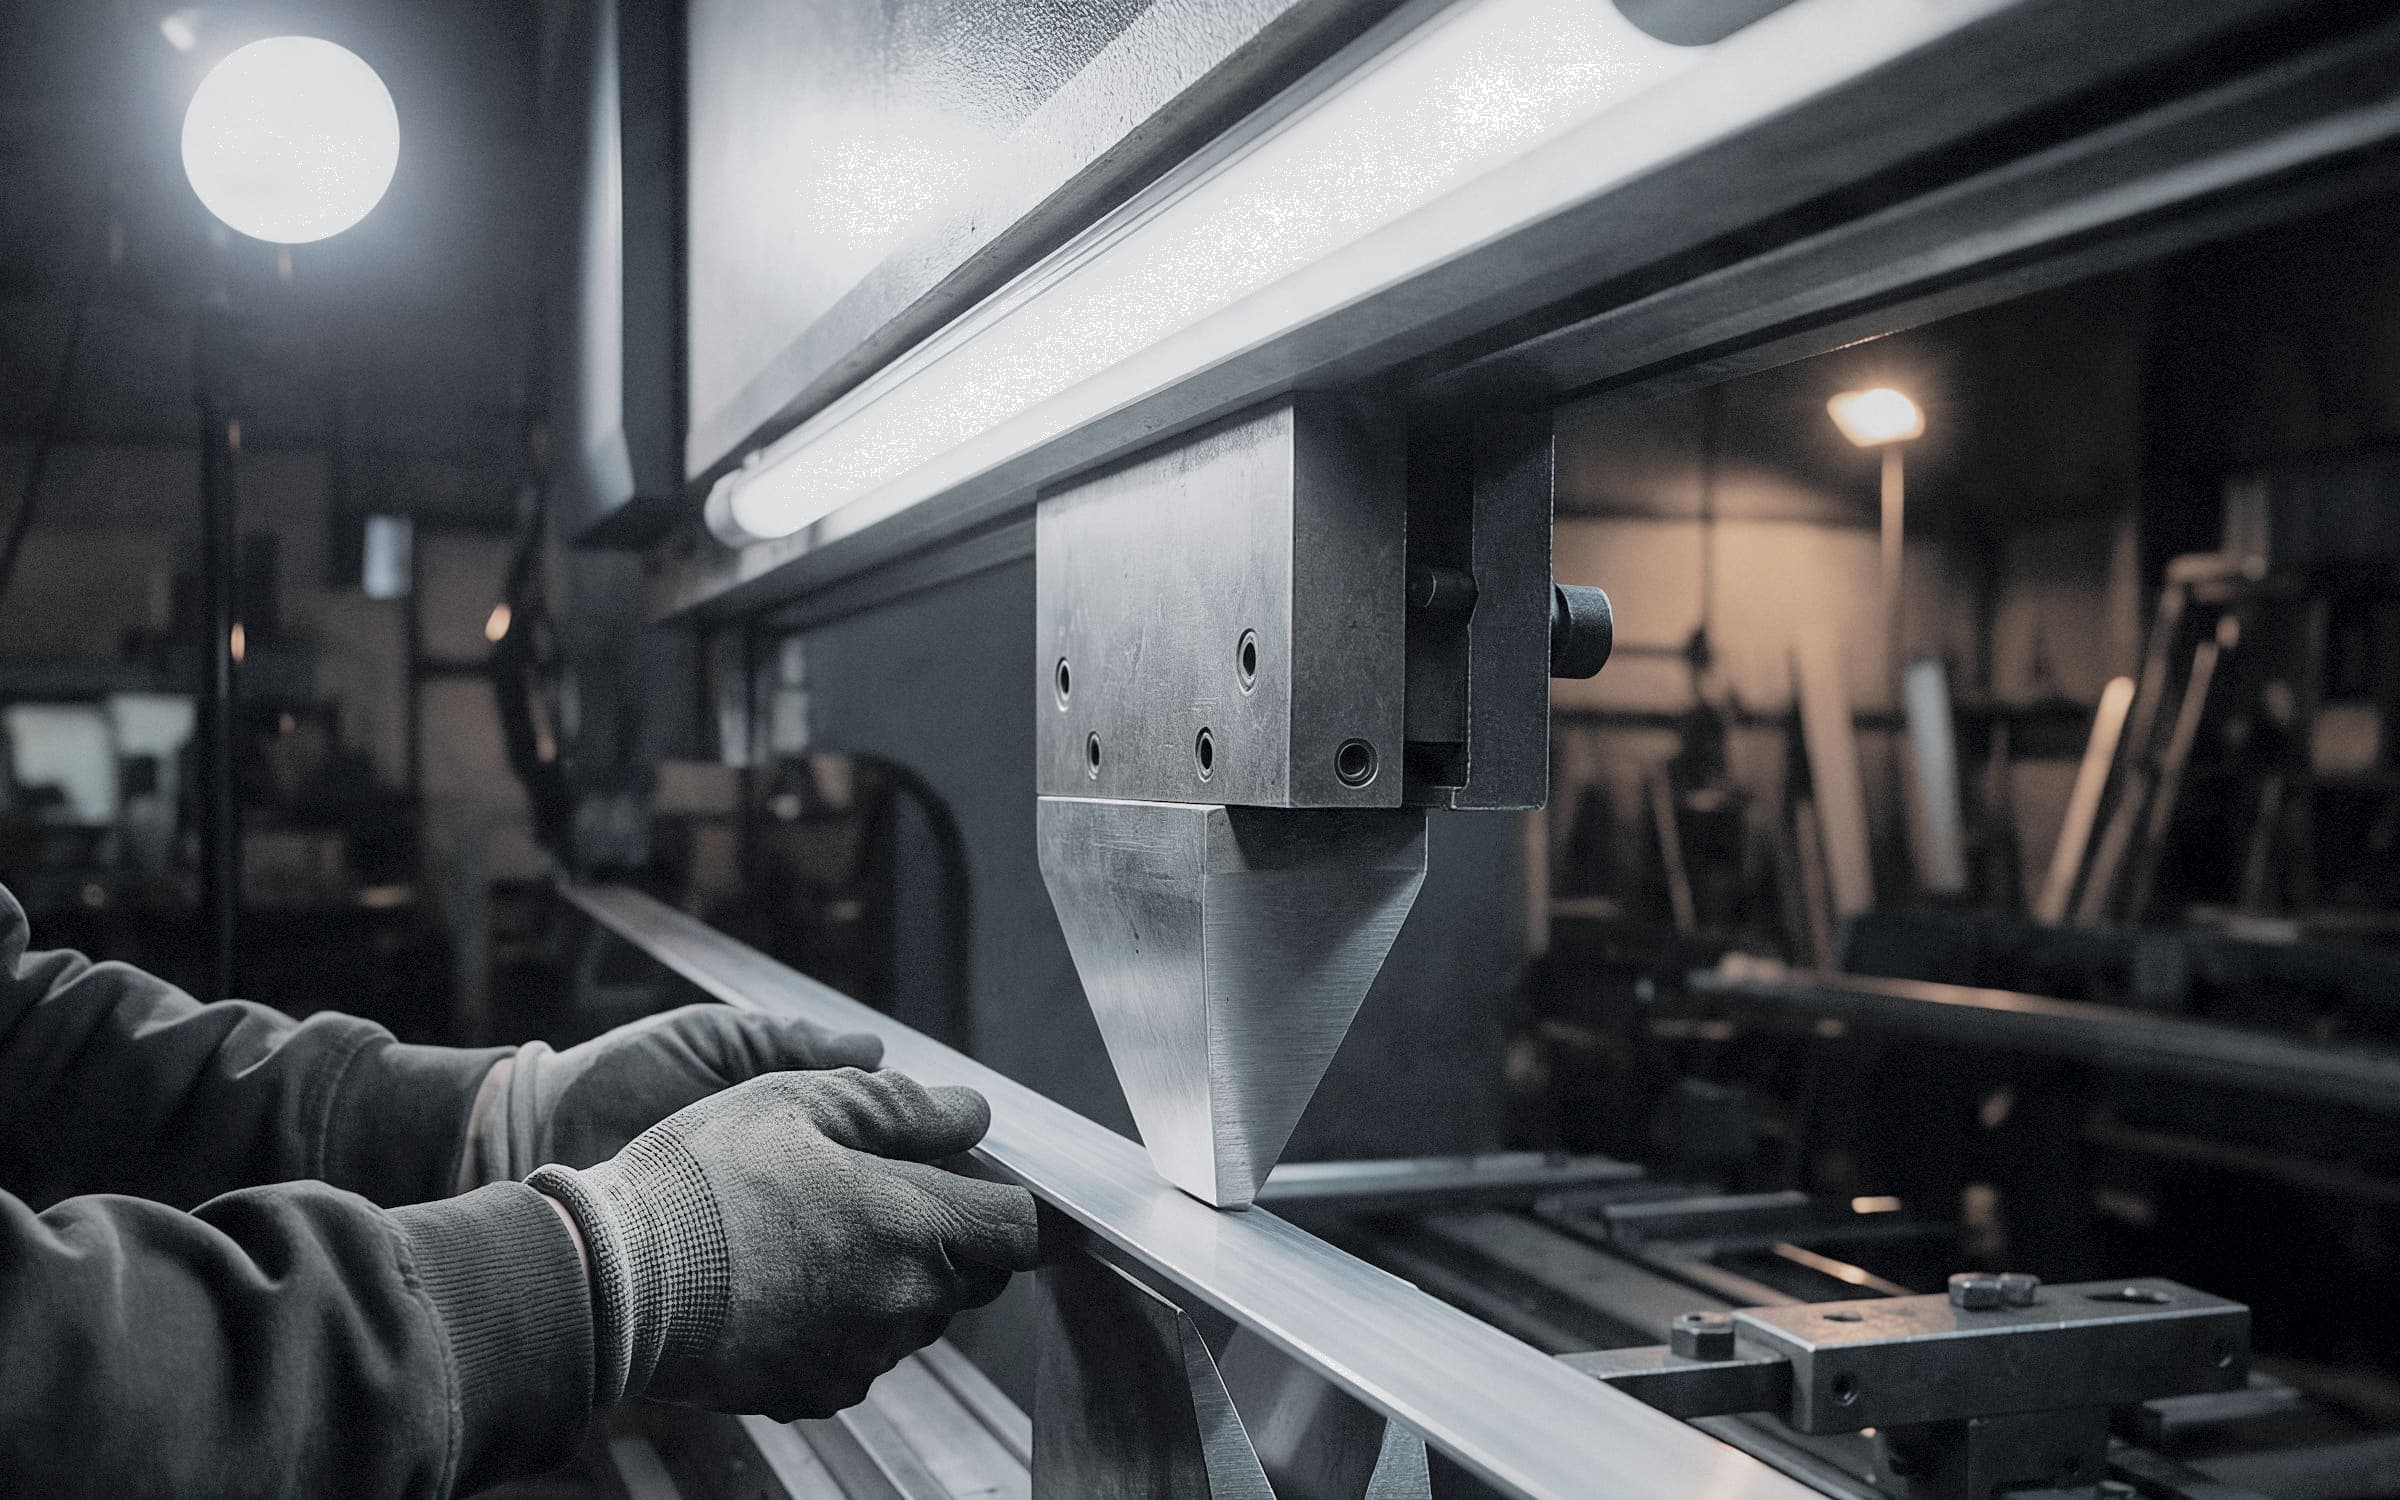
Bends that match the flat pattern, first part.
We unfold your model with our own K-factor, program the bend sequence offline, and measure the first part before the lot runs. Three brakes cover sheet from 0.020 in up to 0.250 in steel at 10 ft.
- 135 T
- 10 FT
- ±0.015 IN
- 135 t, 88 t, 40 t electricFW-M03 to FW-M05
- 10 fton the 135 t
- 0.250 in steelthicker on shorter parts, by quote
- 6-axis on the 135 tflanges and offsets in one setup
- Written offlinethe brake keeps running while we program
- Unfolded with our K-factor, 0.42from your model, checked against your flat
FIG. 02.2 / 135 T BRAKE, SECOND SHIFT
Tolerances, without a callout.
Tighter is possible by quote. Put it on the print and the estimator prices the inspection it needs.
| Feature | Tolerance | Note |
|---|---|---|
| Per bend | ±0.015 in | flange length, outside dimension |
| Bend angle | ±0.5° | ±0.3° on the electric brake |
| Hole to bend | ±0.015 in | when the hole sits 2.5 × t + R or more away |
| Accumulated over 3 bends | ±0.030 in | call out the one that mates |
What runs on this line.
Outside these bars is a conversation, not a no. Call the quote desk with the grade and the thickness.
Check a material against every machinePress brake forming, step by step.
- Unfold
Your model is unfolded with our K-factor and checked against your flat, if you sent one.
- First part
The operator forms one part and measures every flange and angle before the lot runs.
- Lot
The bend program stays on file under your revision, so the next order forms the same way.
The tags on your traveler.
Three changes that lower the price.
No special punch and no setup charge.
Shorter flanges slip off the die and need a second step.
Closer holes stretch into ovals when the flange forms.
A press brake forming package we can price in a day.
- A 3D model (STEP) if you have one. We unfold it ourselves.
- If you send a flat, tell us the K-factor it was drawn with.
- Inside radius on the print, or we form at 1 × t.
- Which flange mates with another part, so we hold that one.
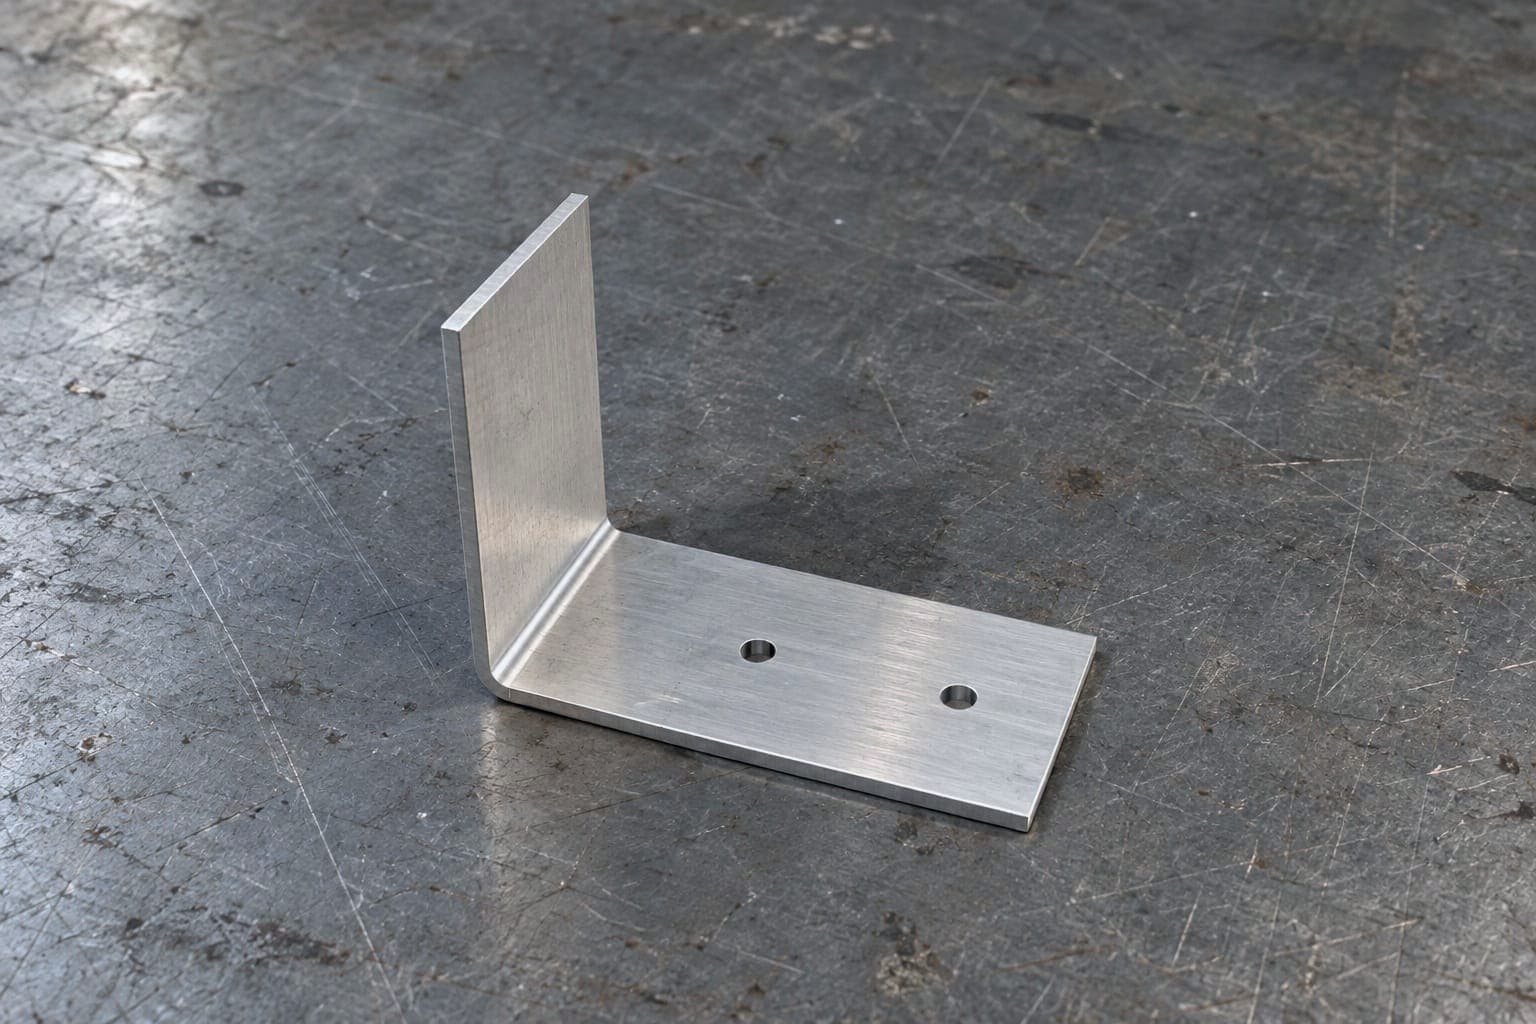
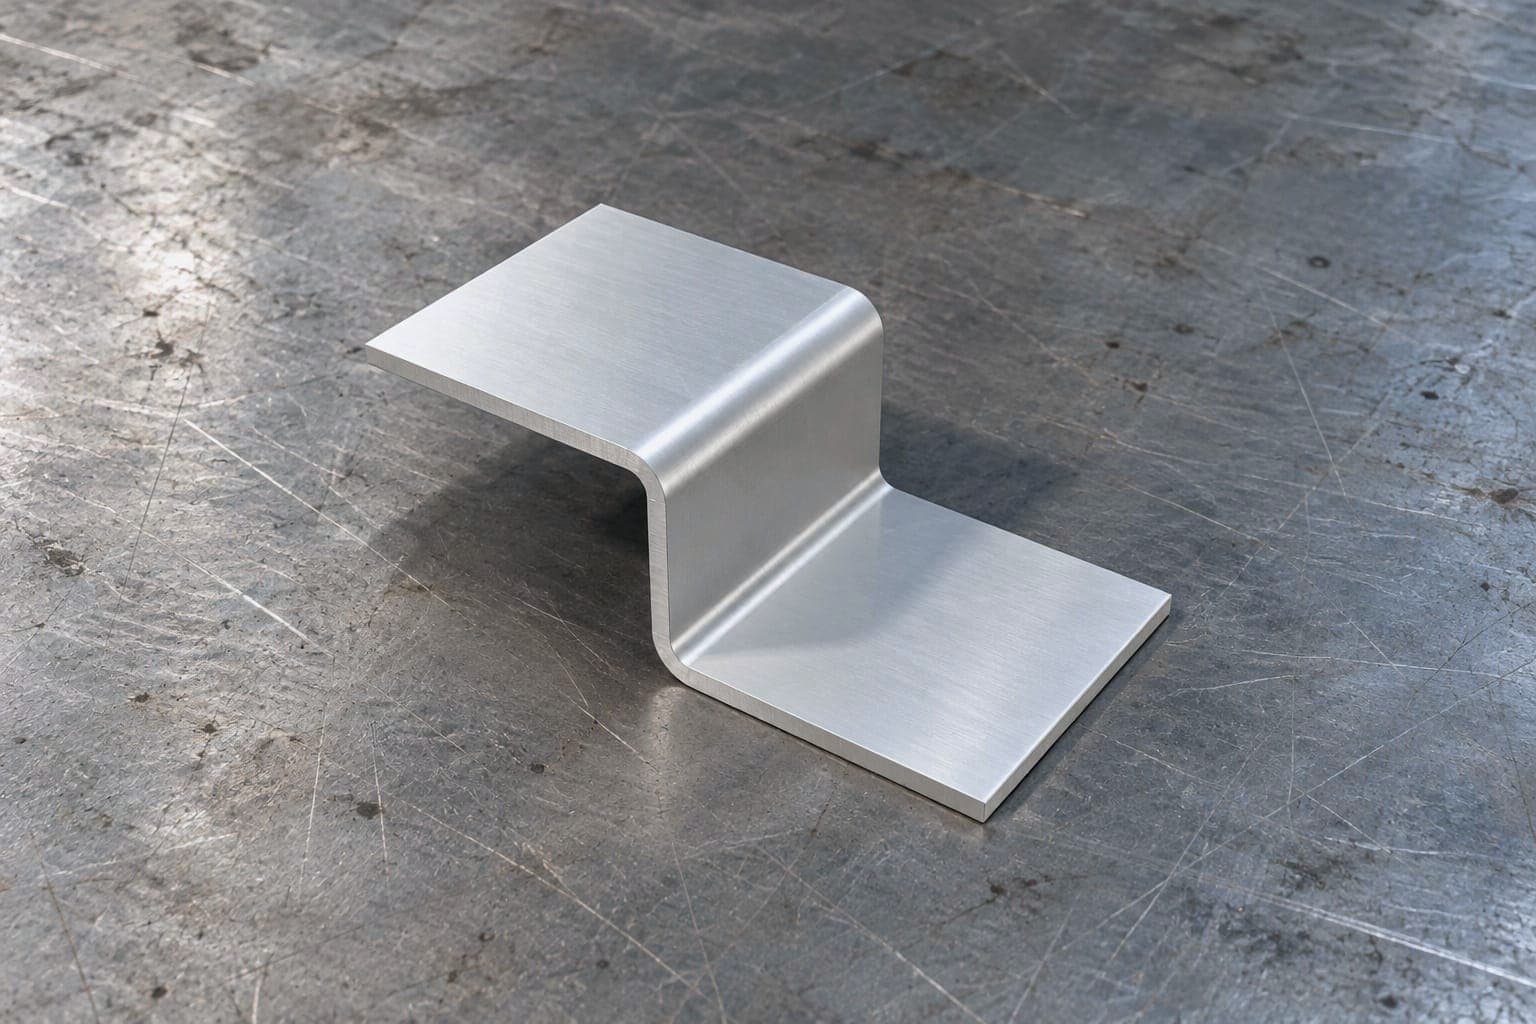
Parts made on this line.
Industries that run on it.
Send a forming job.
A STEP model, the grade and thickness, the radius you need. We unfold it and send back a bend sequence if a flange is short.
DRAWING IN BY 15:00 ET / A PRICED QUOTE THE NEXT BUSINESS DAY