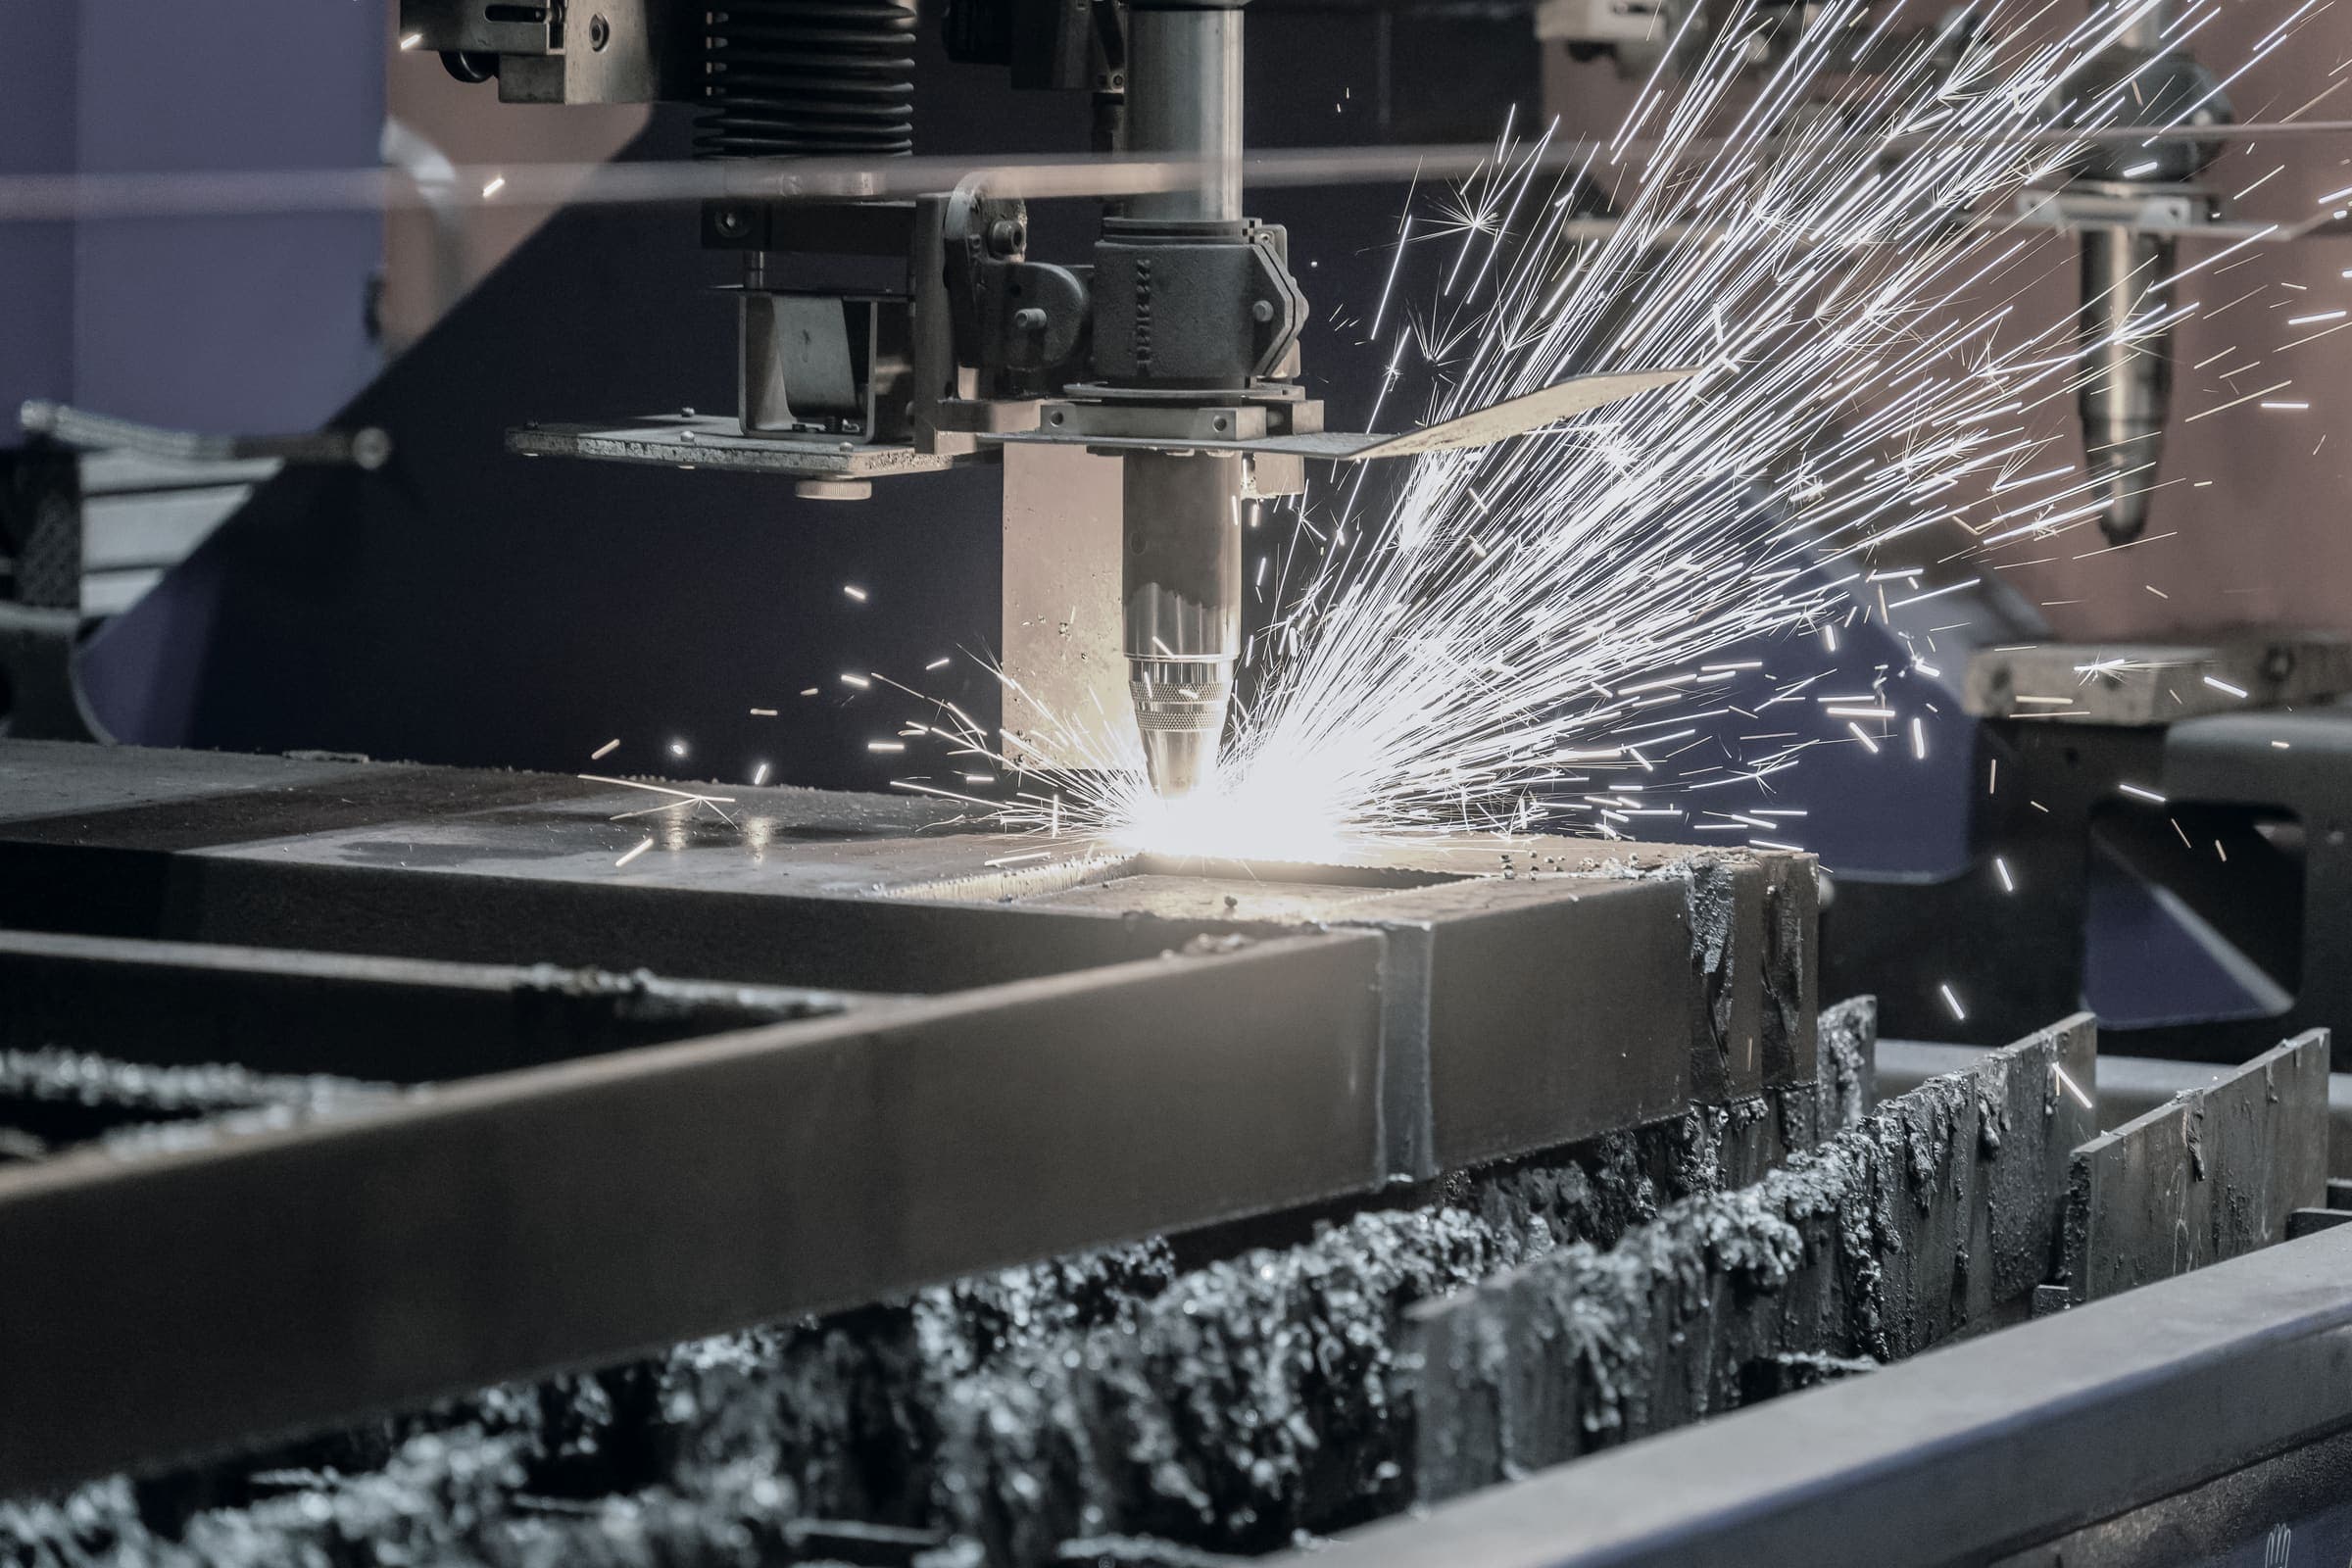
Two fiber lasers. Steel to 0.750 in.
6 kW and 4 kW fiber lasers on 120 × 60 in beds, nested by software and run on both shifts. Parts are deburred on a 37 in wide-belt machine before they leave the cell.
- 6 KW
- 120 × 60 IN
- ±0.010 IN
- 6 kW and 4 kW fiberFW-M01 and FW-M02
- 120 × 60 ina full 5 × 10 ft sheet
- Both, 06:00 to 22:00the 4 kW runs lights-out from its load tower
- 37 in wide-beltevery cut part, both faces
- Common-line cutsshared edges cut once, less scrap
- On requestparts stay in the sheet until we break them out
- 1 × thickness0.040 in minimum in any sheet
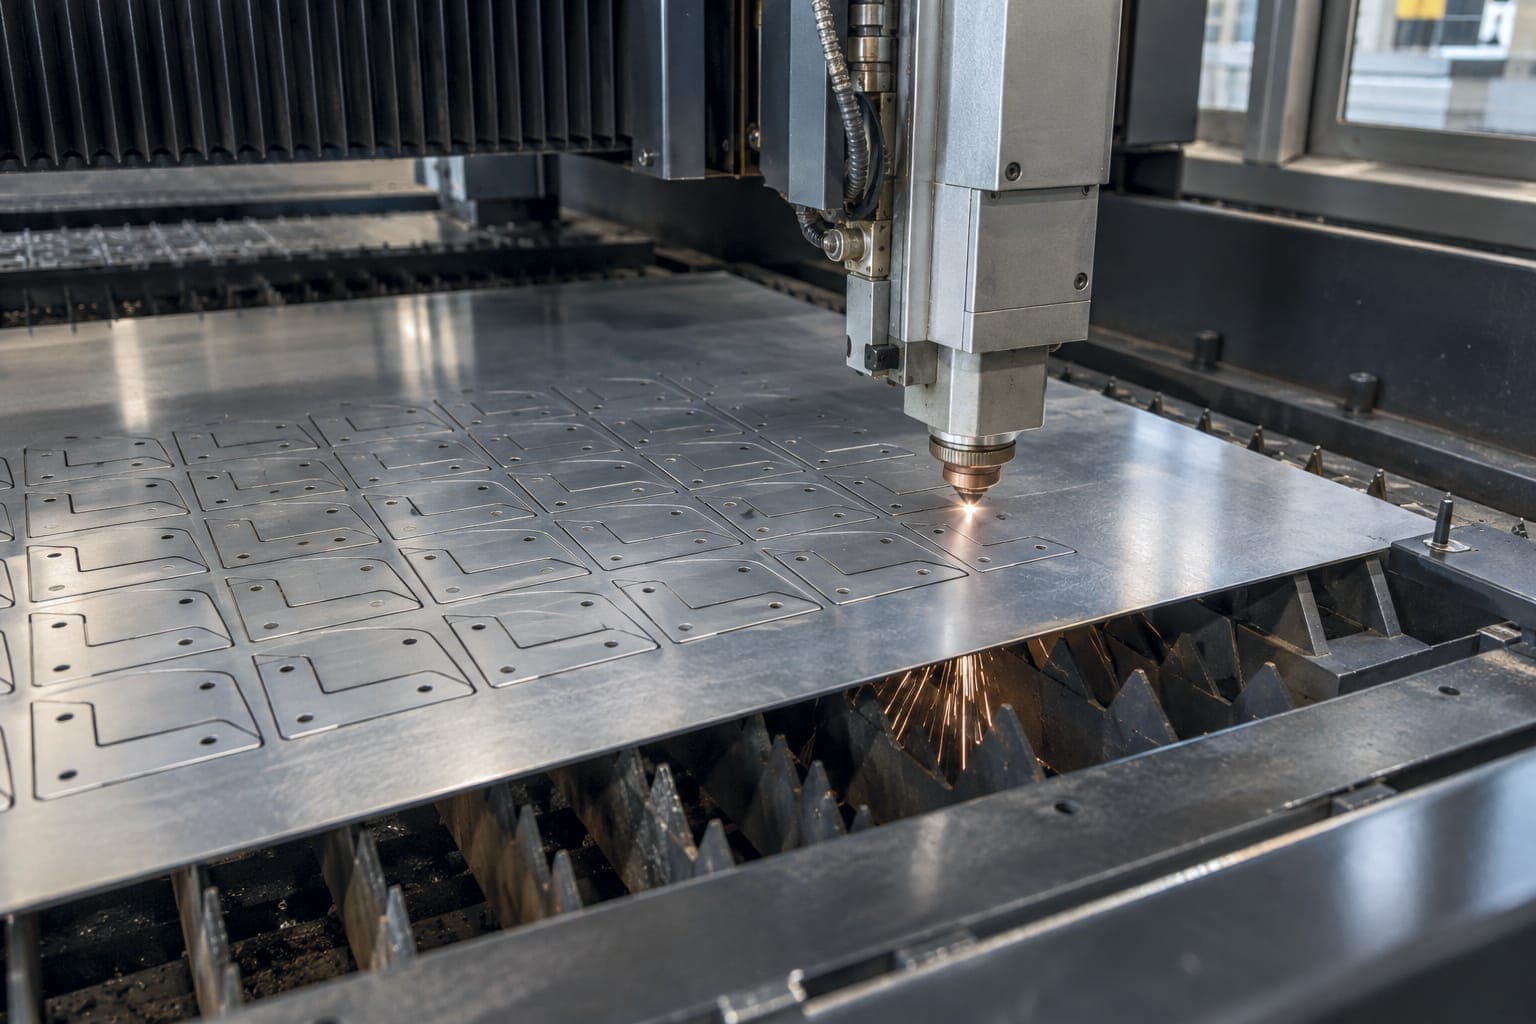
FIG. 02.1 / PIERCING 0.250 IN A36 ON THE SLAT TABLE
Tolerances, without a callout.
Tighter is possible by quote. Put it on the print and the estimator prices the inspection it needs.
| Feature | Tolerance | Note |
|---|---|---|
| Cut features | ±0.010 in | outline, slots and cutouts |
| Hole to hole, same sheet | ±0.005 in | cut in one setup |
| Squareness | 0.010 in over 24 in | checked on the first sheet |
| Edge finish | Deburred, no dross | wide-belt after the cell |
What runs on this line.
Outside these bars is a conversation, not a no. Call the quote desk with the grade and the thickness.
Check a material against every machineLaser cutting, step by step.
- Nest
Your parts share a sheet with others in the same grade and thickness. The nest prints with the traveler.
- First sheet
The first part off the sheet is checked against the print with calipers and pin gauges.
- Break out
Parts come off the skeleton, get their lot tag and go through the wide-belt deburr.
The tags on your traveler.
Three changes that lower the price.
Smaller holes burn out of round; we would drill them as a second step.
Narrow slots trap heat and close up at the bottom.
Parts that share a cut line use less sheet and cost less.
A laser cutting package we can price in a day.
- A DXF of the flat, at 1:1, in inches, one part per file.
- A PDF drawing with the tolerances that matter. We hold ±0.010 in without one.
- Grade and thickness, written out: 304 2B, 0.125 in. Not a gauge number.
- Which face is the show face, if one is.
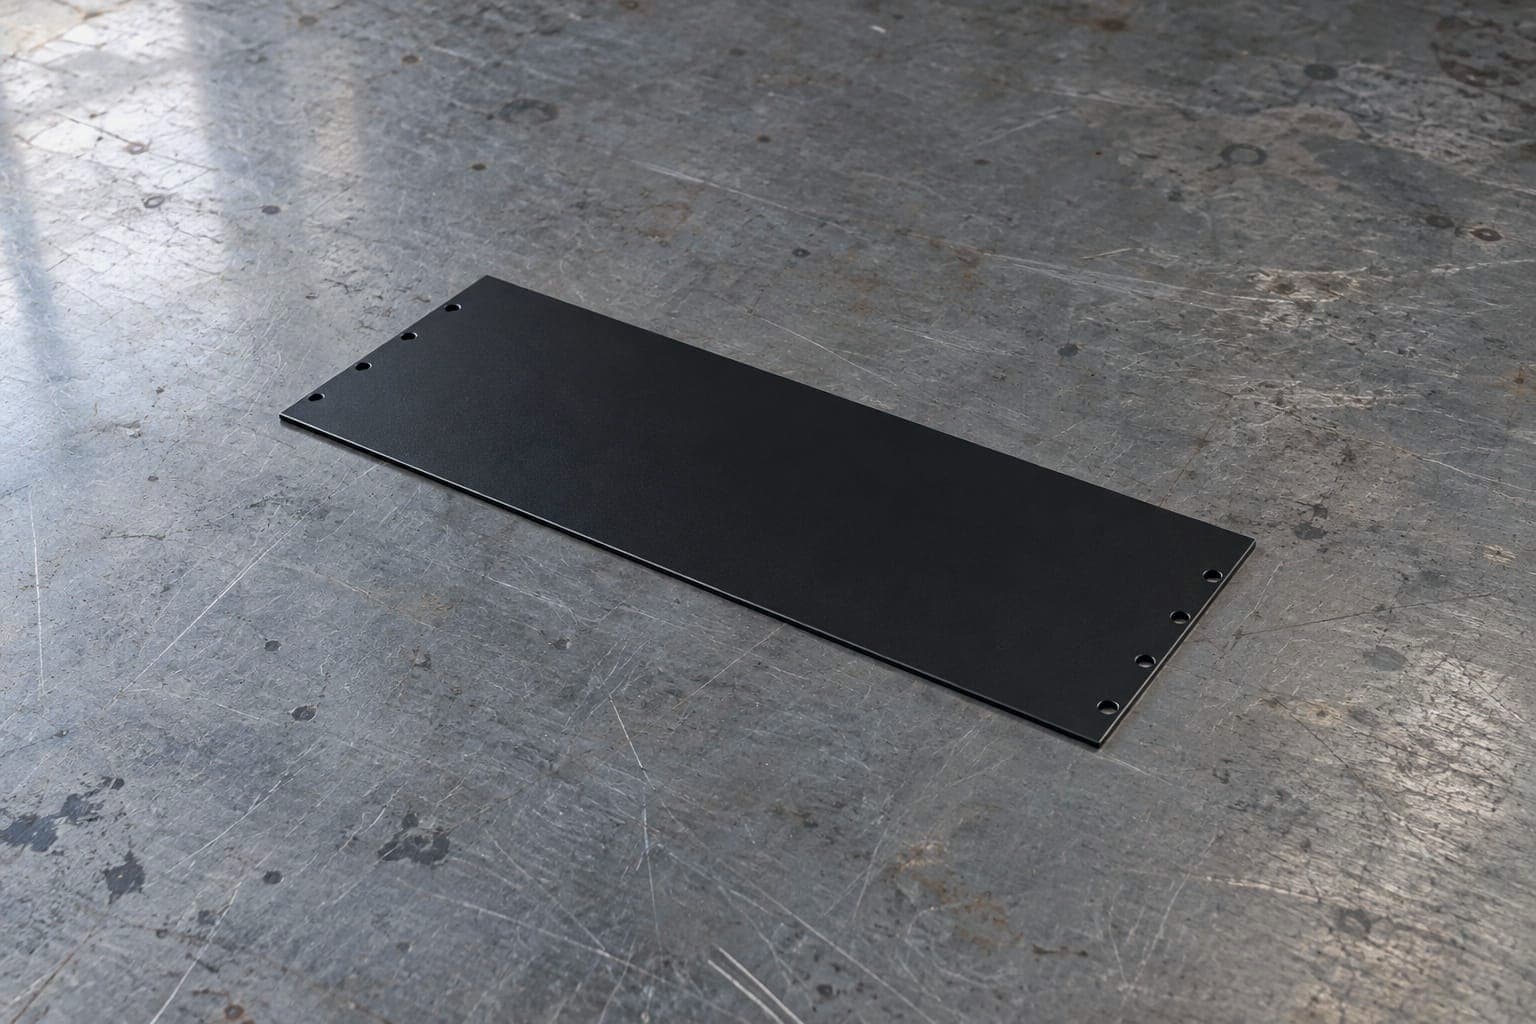
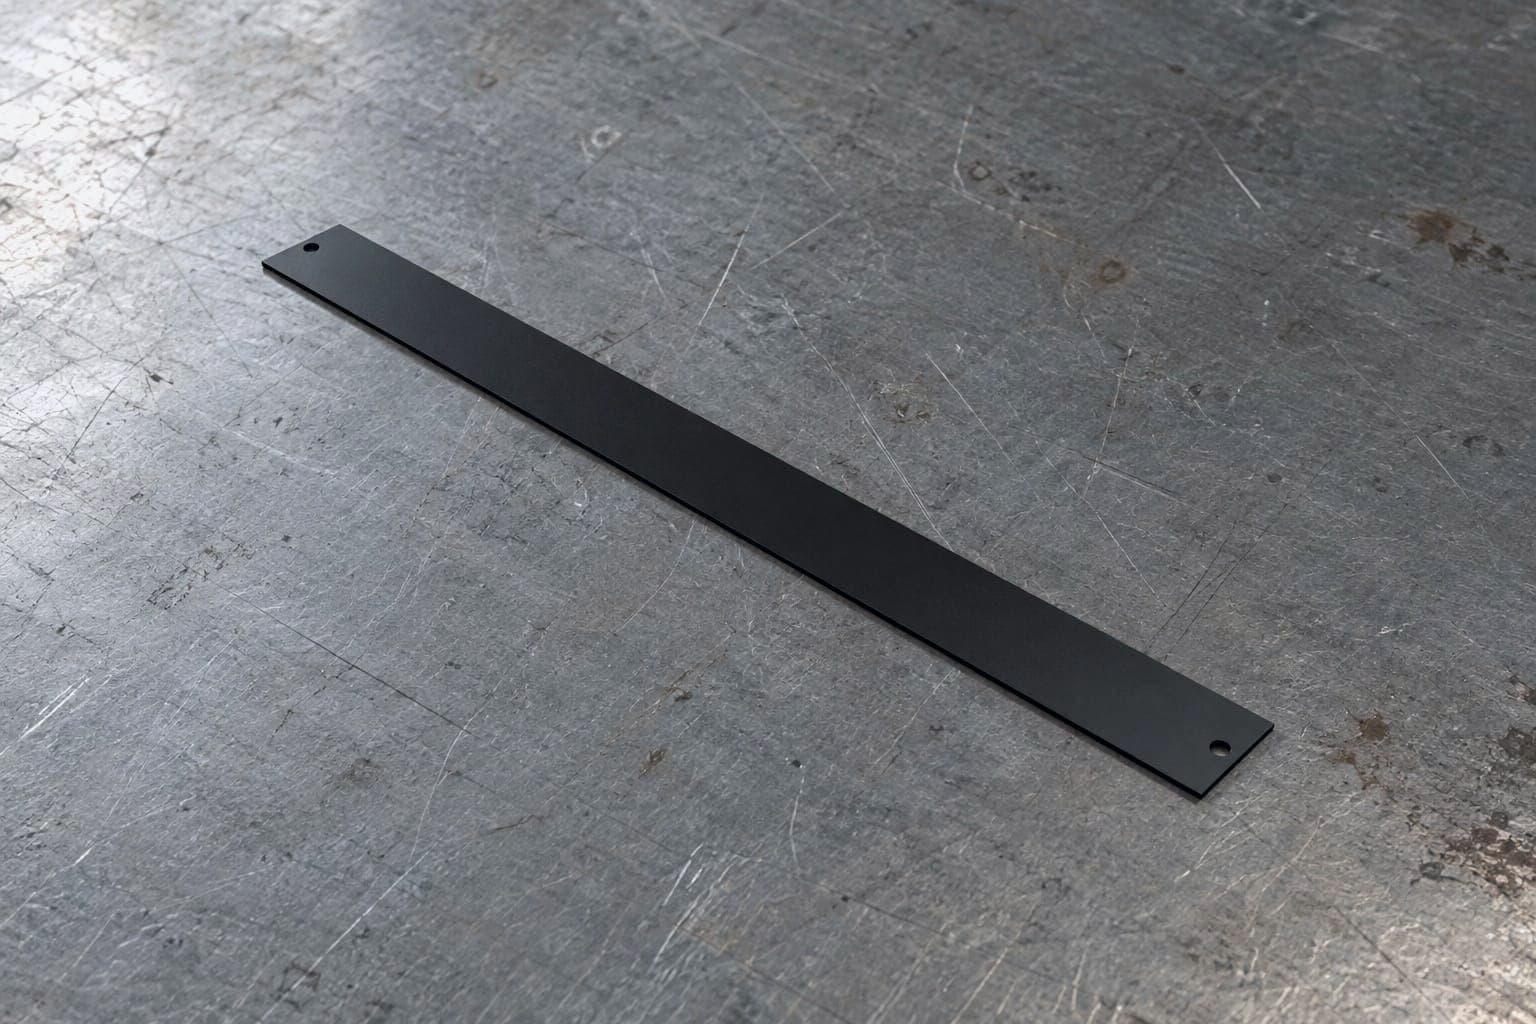
Parts made on this line.
Industries that run on it.
Send a flat. Get a cut date.
DXF plus a PDF drawing, grade and thickness. We price the nest, the deburr and any finish on one line.
DRAWING IN BY 15:00 ET / A PRICED QUOTE THE NEXT BUSINESS DAY