Eight rules that make parts cost less.
From the brake and the laser. Follow them and the quote drops. Break them and we call before we cut.
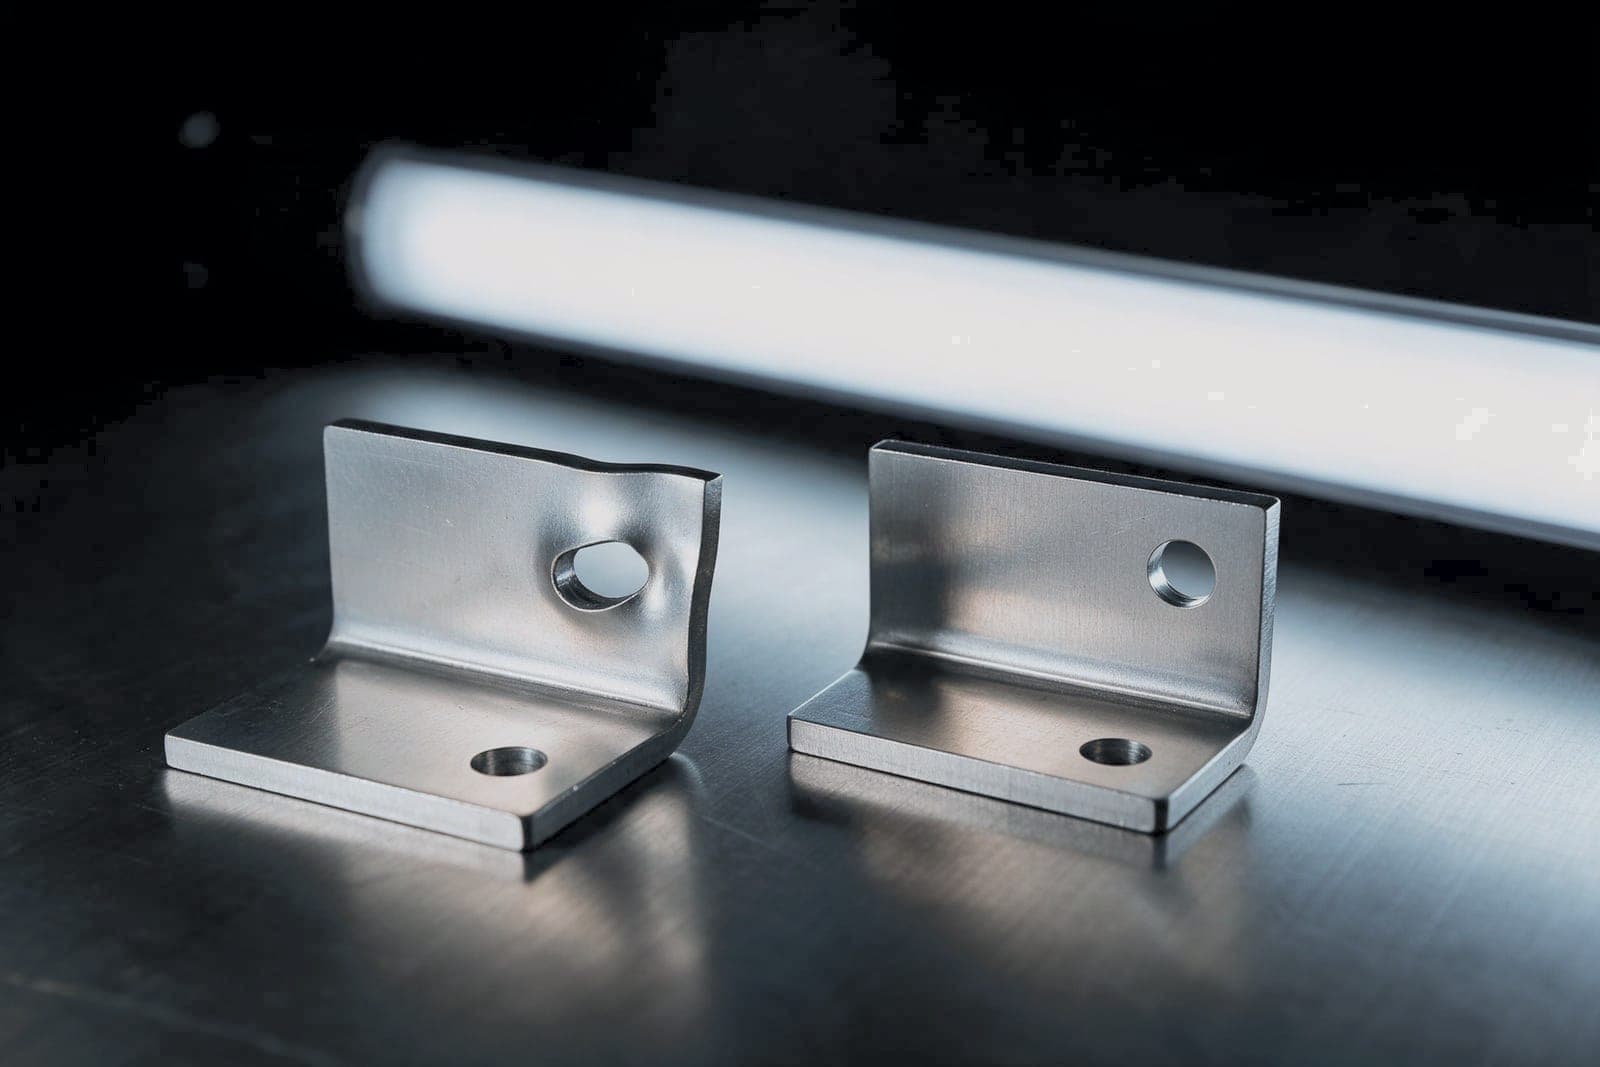
Inside bend radius = 1 × t.
Standard tooling forms a 1 × t inside radius in steel, 304 and 5052. 6061-T6 needs 1.5 × t or it cracks on the outside of the bend.
Standard tooling, no special punch, no setup charge.
Flange at least 4 × t.
0.063 in sheet: 0.25 in minimum flange. 0.125 in: 0.50 in. At 0.250 in, 1.00 in.
Shorter flanges slip off the die and need a second operation.
Hole to edge at least 2 × t.
0.125 in sheet: the edge of the hole sits 0.25 in or more from the edge of the part.
Closer holes bulge the edge and fail inspection.
Hole to bend at least 2.5 × t + R.
0.125 in sheet with a 0.125 in radius: 0.44 in from the bend line to the edge of the hole.
Closer holes stretch into ovals when the flange forms.
Smallest laser hole = t.
0.040 in minimum in any thickness. In 0.250 in plate, 0.250 in.
Smaller holes burn out of round, and we would drill them as a second step.
Bend relief: width at least t, depth R + t.
Where a bend runs into an edge, a small notch lets the metal move.
No tearing at the corner and no hand finishing.
Hardware: tell us the part number.
Self-clinching nuts and studs need a minimum sheet thickness and edge distance. We check the fastener against your sheet before we quote.
No pressed-in hardware that spins out.
Call out what matters.
±0.010 in on cut features and ±0.015 in per bend are standard. Tolerances stack across bends. Tighten only the dimensions that mate.
Every tight tolerance adds an inspection step to every part.
We unfold with K = 0.42.
That is the K-factor on our tooling. Send a 3D model and we unfold it ourselves; send a flat and we check it against the model. If your flat was drawn with a different K-factor, tell us the number and we will match the formed part, not the flat.
Press brake forming in detailWhat is on the rack today.
Stock ships on the quote's lead time. Anything marked 3 to 5 days adds that to the ship date. A dot means we do not buy it in that thickness.
| Grade / in | 0.040 | 0.063 | 0.090 | 0.125 | 0.188 | 0.250 | 0.375 | 0.500 | 0.750 |
|---|---|---|---|---|---|---|---|---|---|
| 5052-H32 | STOCK | STOCK | STOCK | STOCK | STOCK | STOCK | 3 TO 5 D | 3 TO 5 D | · |
| 6061-T6 | 3 TO 5 D | 3 TO 5 D | 3 TO 5 D | 3 TO 5 D | 3 TO 5 D | STOCK | STOCK | STOCK | STOCK |
| 304 2B | STOCK | STOCK | STOCK | STOCK | STOCK | STOCK | 3 TO 5 D | 3 TO 5 D | · |
| 316L 2B | 3 TO 5 D | STOCK | 3 TO 5 D | STOCK | 3 TO 5 D | 3 TO 5 D | 3 TO 5 D | 3 TO 5 D | · |
| A36 HRPO | · | · | · | STOCK | STOCK | STOCK | STOCK | STOCK | STOCK |
| 1018 CRS | STOCK | STOCK | STOCK | STOCK | 3 TO 5 D | · | · | · | · |
| 303 bar | Hex and round bar to 2 in, in stock | ||||||||
Not sure a rule applies? Send the drawing.
The estimator flags any feature that breaks a rule, says what it costs to keep it, and suggests the change that removes the cost. Your call either way.