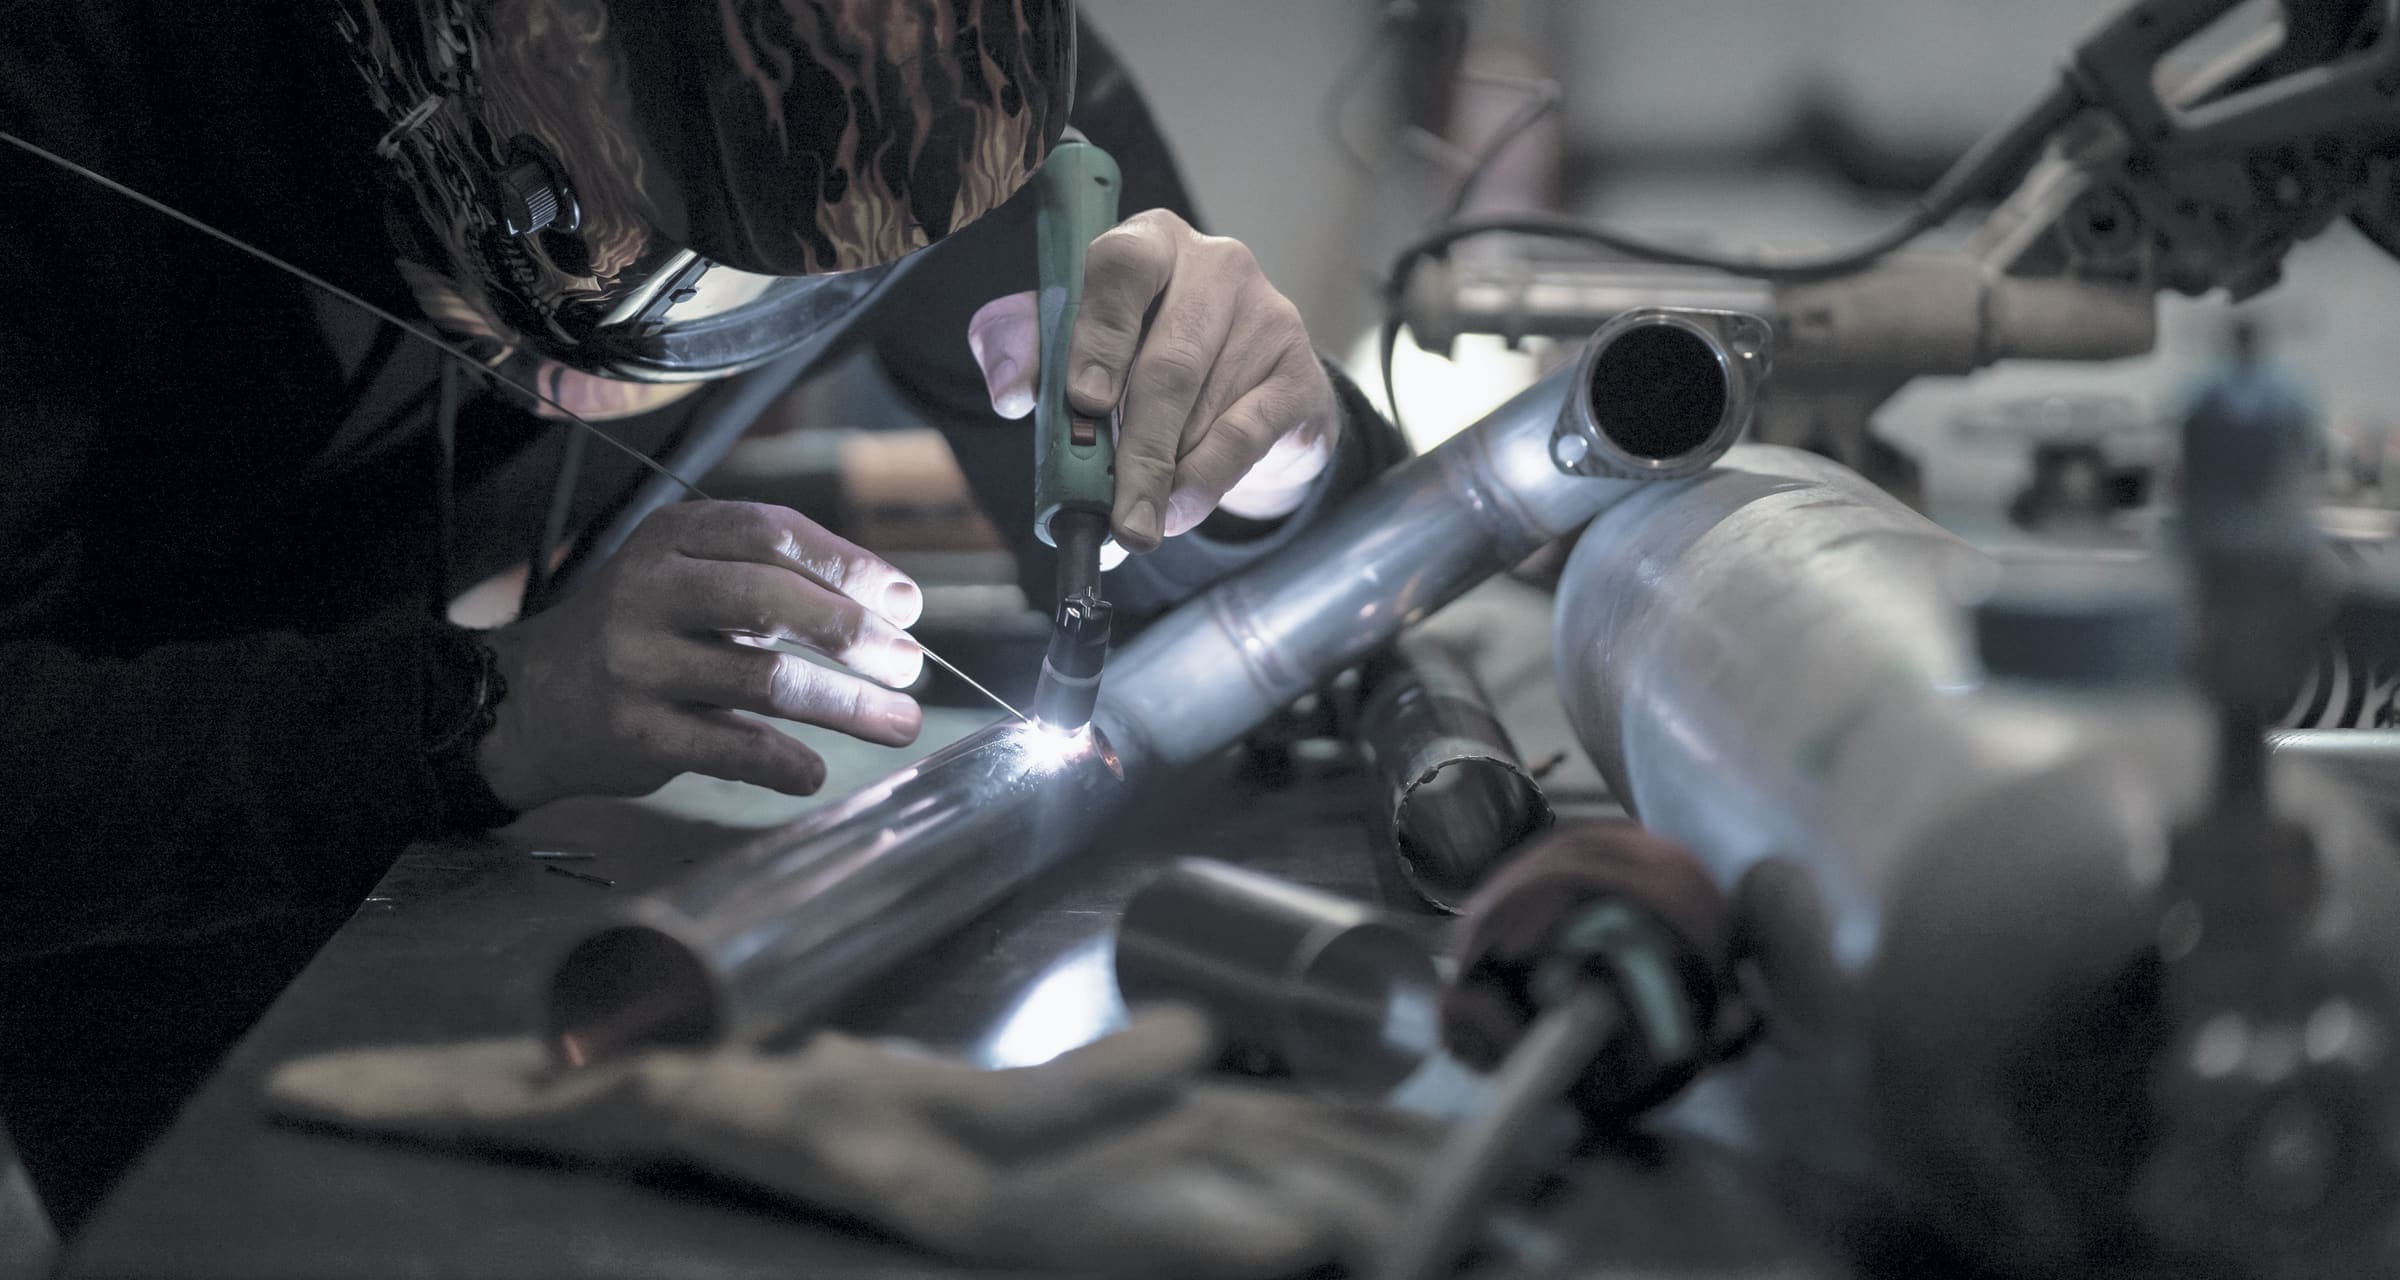
Welded in fixtures, checked on the plate.
TIG, pulse MIG and spot welding in two cells, each with an 8 × 4 ft fixture table. Weldments are checked for flatness on the surface plate before they go to finish.
- 2
- 8 × 4 FT
- 0.030 IN
- 2, curtainedFW-M10 and FW-M11
- TIG, pulse MIG, spotspot on FW-M12
- 8 × 4 ft eachsteel, drilled on a grid
- 0.040 to 0.500 insteel, stainless and aluminum
- Flatness on the surface platebefore the part goes to finish
- Weld record on requestprocedure and welder by job
FIG. 02.4 / CELL 1, TIG ON 304 TUBE
Tolerances, without a callout.
Tighter is possible by quote. Put it on the print and the estimator prices the inspection it needs.
| Feature | Tolerance | Note |
|---|---|---|
| Flatness after welding | 0.030 in over 24 in | checked on the granite plate |
| Leg angle after welding | ±0.5° | corrected on the fixture |
| Fillet size | Per print, ±0.030 in | visual and gauge |
| Heat tint on stainless | Removed | passivate or electropolish after |
What runs on this line.
Outside these bars is a conversation, not a no. Call the quote desk with the grade and the thickness.
Check a material against every machineWelding, step by step.
- Fixture
Parts are clamped to a fixture built for the part, so every one in the lot welds the same.
- Sequence
Stitch welds alternate side to side to keep heat from pulling the part.
- Plate
Every weldment is checked flat on the surface plate before it goes to finish.
Three changes that lower the price.
Parts locate themselves, so there is less fixture to build.
No grinding on a face the customer sees.
Less heat, less distortion, less time.
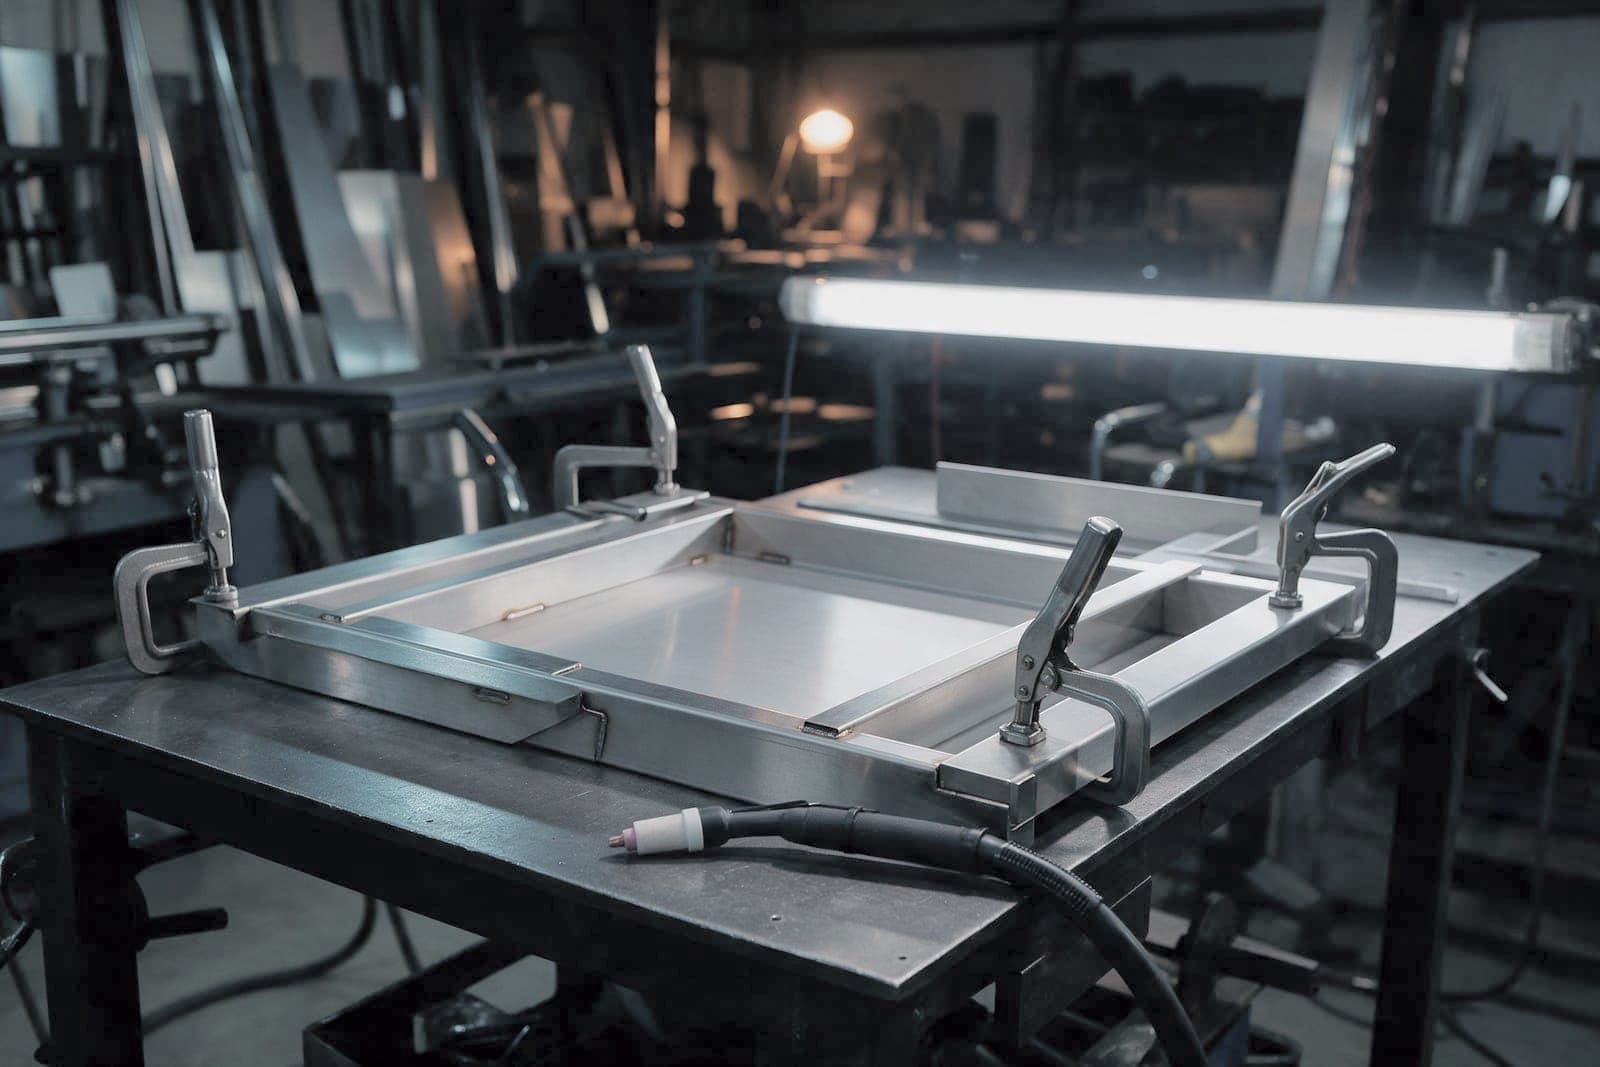
A welding package we can price in a day.
- The weld symbols on the drawing, or a note on what must be sealed.
- Which faces are finished faces.
- Flatness or angle requirements after welding.
- Whether you need a weld record in the box.
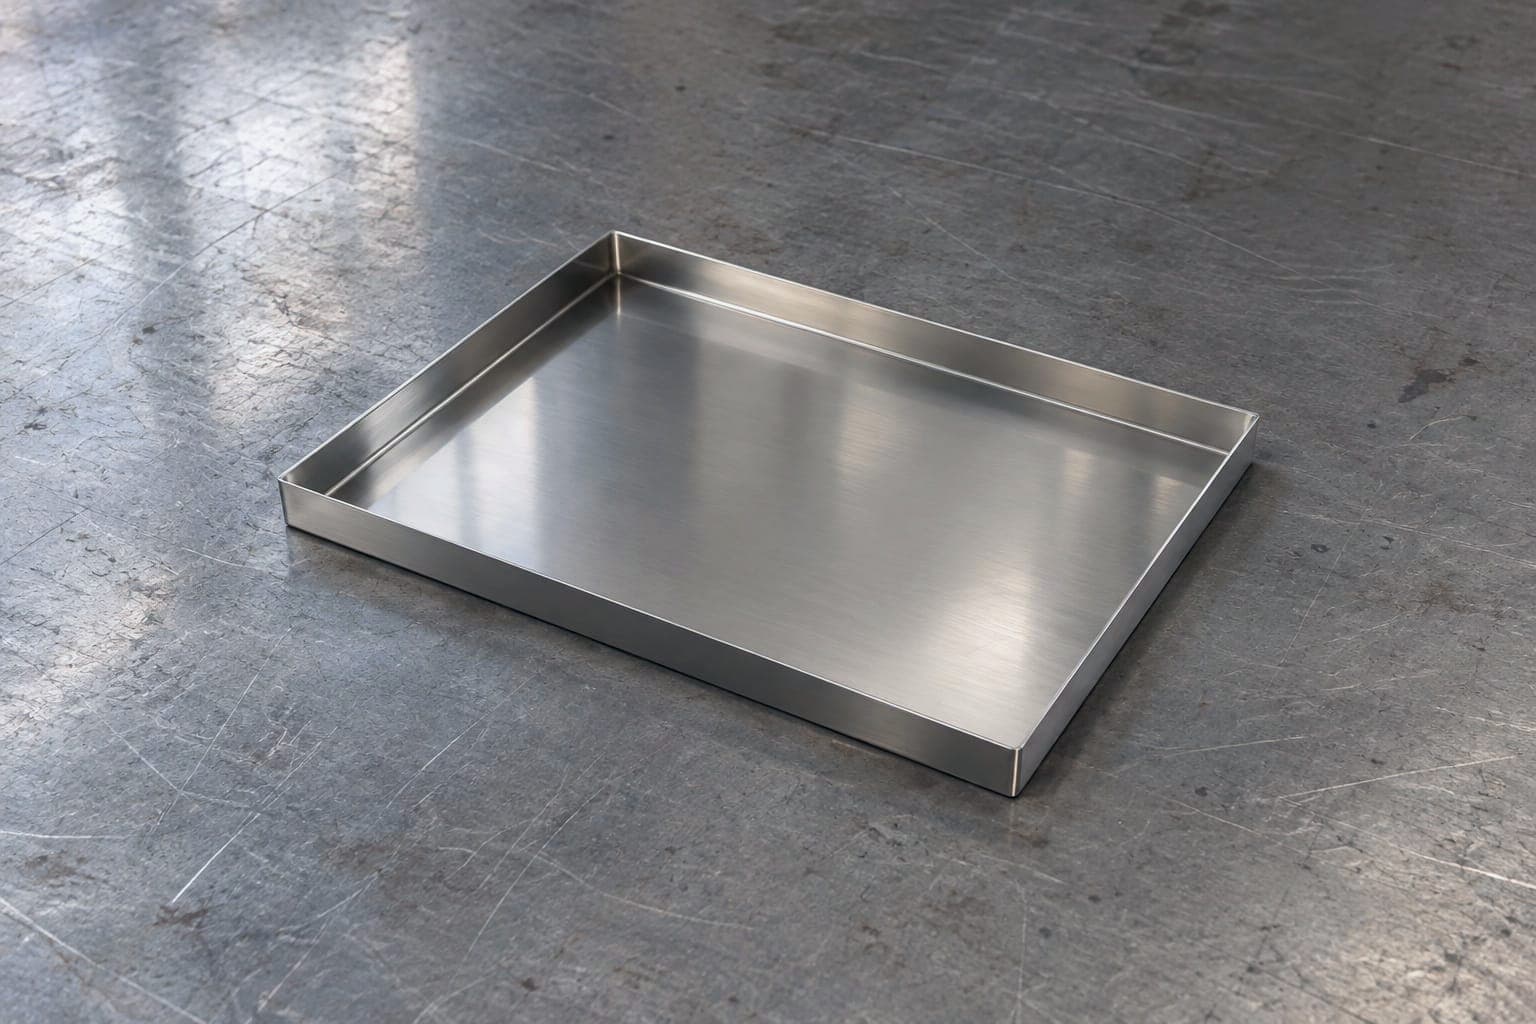
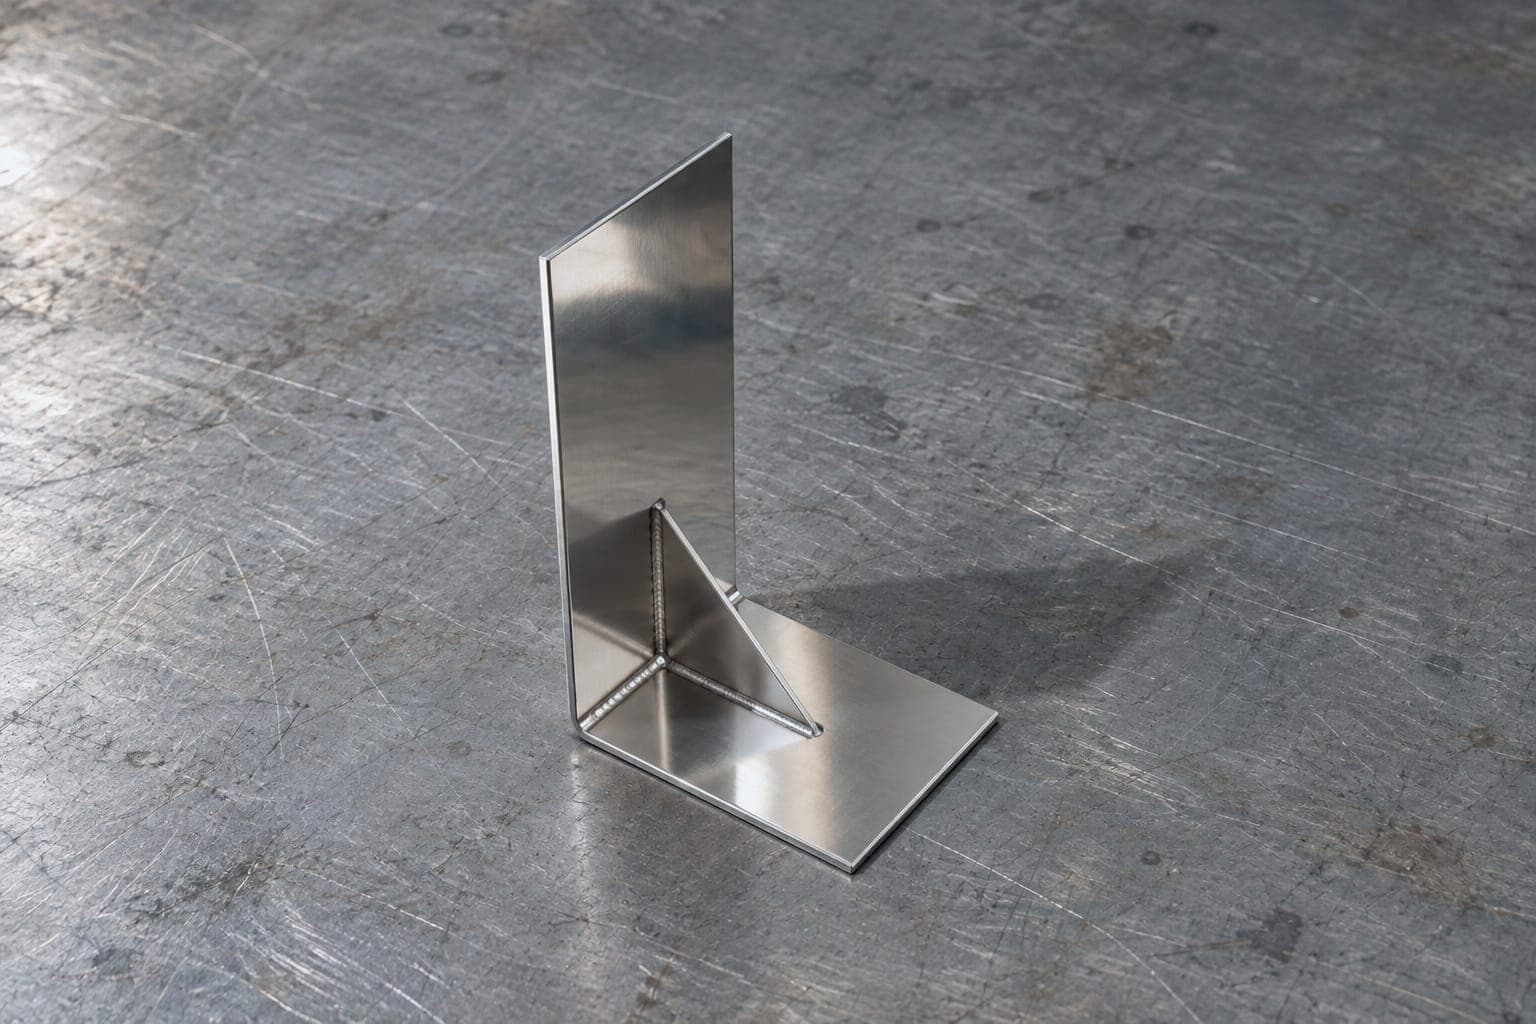
Parts made on this line.
Industries that run on it.
Send a weldment.
The drawing with weld symbols, the material and the flatness you need. We quote the fixture once and keep it for the next lot.
DRAWING IN BY 15:00 ET / A PRICED QUOTE THE NEXT BUSINESS DAY